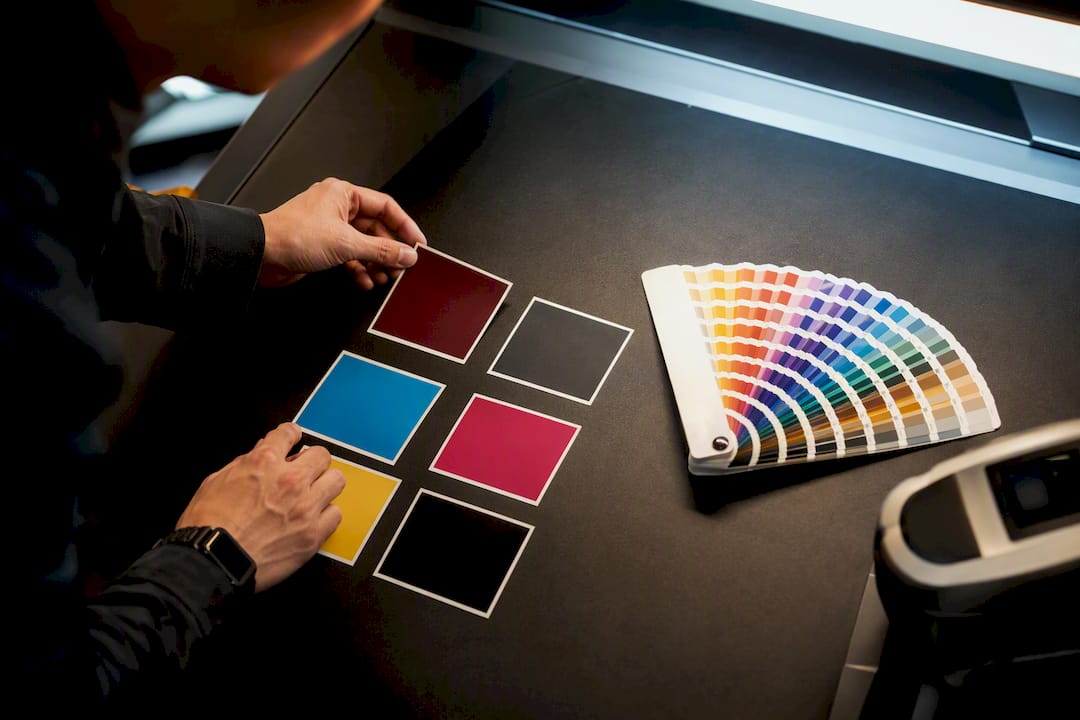
Pick Pantone when a color has to survive the trip from screen to shelf without drifting: logos, brand marks, metallics, fluorescents, or anything printed on colored or uncoated stock. Pick CMYK for photography, gradients, and full-color imagery where a slight shift is invisible to the eye. If a project needs both, run CMYK for imagery and add one or two spot inks for the logo. Either way, your next move is the same: soft-proof against the printer’s ICC profile and check the Delta-E before you sign off.
**TL;DR:** Pantone colors provide consistent and exact matches for brand-critical elements like logos, metallics, fluorescents, and applications on uncoated or colored substrates, but require proper documentation and proofing to ensure accuracy. CMYK is suitable for photographic images, gradients, and large-format graphics, yet its narrower gamut often prevents exact replication of saturated or metallic Pantone colors, especially when converting. Using ΔE measurements to compare Pantone simulations with CMYK builds helps determine whether a color match is acceptable, with 2 or less being imperceptible and above 5 considered a visible mismatch. Proper workflow includes early declaration of color intent, soft-proofing against ICC profiles, physical proof approval, and detailed documentation to prevent costly reprints and color inconsistencies. Converting Pantone to CMYK is inherently lossy, with most Pantone hues sitting outside CMYK’s gamut, especially metallics and fluorescents, making initial color selection and substrate choice critical.
Yuanpackaging
Explore Yuan Packaging
Table of Contents
- Pantone vs CMYK: What Actually Separates Them
- How CMYK Works: Halftones, Dot Gain, and Device Drift
- What Pantone Actually Is: Premixed Ink, Not a Filter
- Gamut and Delta-E: How to Judge a CMYK Match
- When to Use Pantone vs CMYK for Printing
- The File Prep and Proofing Workflow That Prevents Reprints
- What a Packaging Manufacturer Should Deliver on Color
- Why Brand Color Consistency Depends on More Than the Ink
- A Short History of Two Very Different Color Systems
- Spot Color vs Process Printing: The Technical Divide
- Why Converting Pantone to CMYK Rarely Works Perfectly
- Choosing the Right Pantone Color for a CMYK-Friendly Result
- How Lighting Changes What You’re Actually Approving
- Give Your Packaging the Color Fidelity It Deserves
- What This Debate Gets Wrong
- Sources
- FAQ
Pantone vs CMYK: What Actually Separates Them
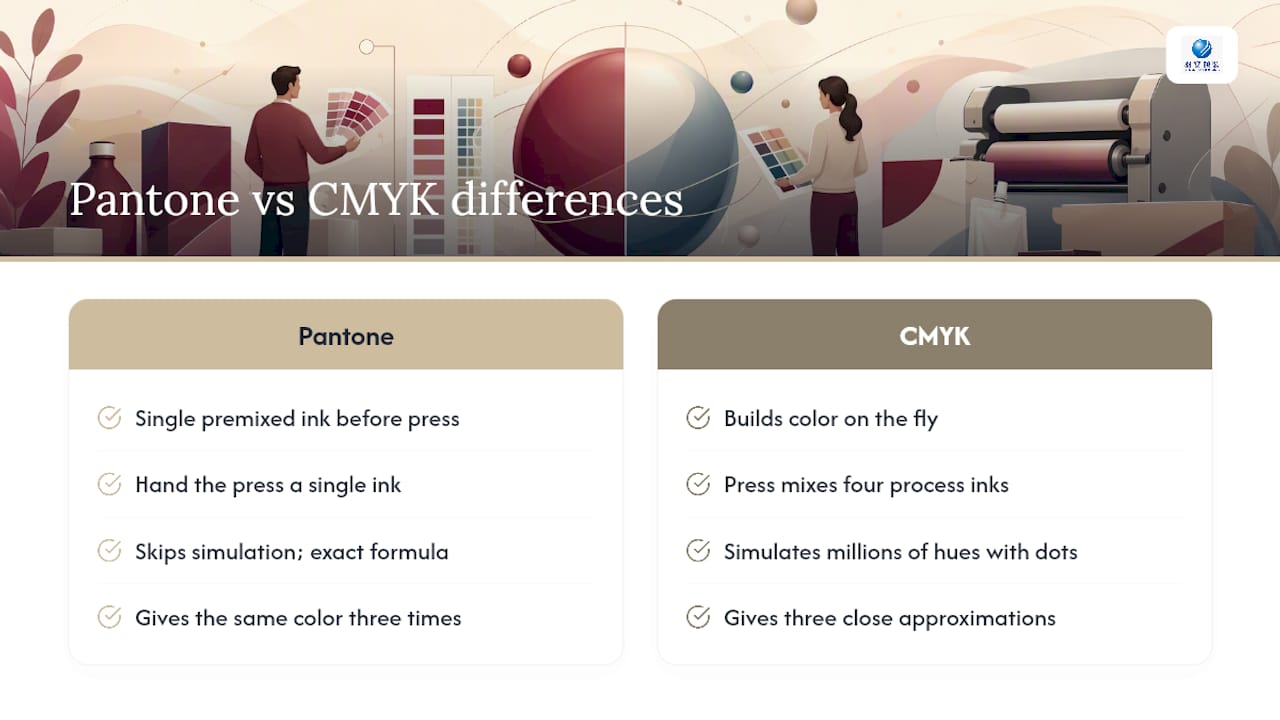
The confusion between these two systems comes down to one word: consistency. CMYK builds color on the fly, mixing four process inks through tiny dots to simulate millions of hues. Pantone skips the simulation and hands the press a single ink, mixed to an exact formula before it ever touches a roller. That difference sounds small until you’re matching a logo across a folding carton, a rigid box, and a pressure-sensitive label made on three different presses. CMYK will give you three close approximations. Pantone, run correctly, gives you the same color three times.
Neither system is “better” in the abstract. They solve different problems, and most packaging jobs need both at once, which is exactly why the decision gets treated as a binary when it should be treated as a division of labor.
How CMYK Works: Halftones, Dot Gain, and Device Drift
CMYK is a subtractive process. Cyan, magenta, yellow, and black inks absorb light rather than emit it, and the eye blends tiny halftone dots into what looks like a continuous color. Those dots are screened at specific angles and sizes, and how much a dot spreads on press (dot gain) depends on paper absorbency, ink viscosity, and press speed.
That’s what makes CMYK a **device-dependent** system. The same file can print noticeably differently on two presses, two paper stocks, or even two shifts with the same operator, which is why ICC profiles and soft-proofing exist to keep expectations aligned with reality before a job ever hits the plate.
Prepress teams manage this drift with a few standard controls:
- Total ink coverage limits, typically capped around 300% to 340% to prevent oversaturation and slow drying.
- Rich black recipes (layering CMY under 100% K) for deep, non-mottled blacks.
- Screening angle adjustments to avoid moiré interference in fine patterns.
- Extended-gamut printing (CMYKOG or CMYKOGV, adding orange, green, and sometimes violet) to reach hues standard CMYK can’t touch.
What Pantone Actually Is: Premixed Ink, Not a Filter
Pantone, often shorthand for the Pantone Matching System (PMS), is a library of premixed spot inks, each with a standard formula and a reference code. A designer doesn’t approximate Pantone 186 C, they specify it, and the printer mixes that exact ink rather than simulating it with four process colors. That’s the entire mechanism behind Pantone’s consistency claim: removing the guesswork that comes from device-dependent mixing.
Every Pantone color ships in two formulations that behave differently on the same substrate:
- *Coated ©:** formulated for glossy or coated stock, where ink sits on the surface and reads brighter and more saturated.
- *Uncoated (U):** formulated for absorbent, uncoated stock, where ink soaks in slightly and reads duller and warmer.
Spot inks also do things CMYK physically cannot: true metallics, fluorescents, and several high-chroma reds, blues, and greens sit outside the CMYK gamut entirely. The Pantone Bridge guide maps each solid Pantone color to its nearest CMYK simulation, which is useful for previewing a conversion but should never be mistaken for a guarantee that the simulation will pass inspection.
Gamut and Delta-E: How to Judge a CMYK Match
Color gamut is simply the range of colors a system can reproduce, and CMYK’s range is narrower than Pantone’s spot-ink library. More than half of all Pantone colors fall at least partially outside the standard CMYK gamut, according to Fujifilm’s printing team, which means a straight conversion often lands close but not identical. Neons, certain saturated blues and reds, and every metallic fall firmly outside what four process inks can fake.
Judging “close enough” isn’t a matter of squinting at a monitor. The print industry uses Delta-E (ΔE), a numeric measure of the visual distance between two colors, ideally calculated with the CIEDE2000 formula for the most perceptually accurate result.
| ΔE range | What it means in practice |
|---|---|
| Below 2 | Generally imperceptible to the human eye |
| 2 to 5 | Small difference, may be noticeable side by side |
| Above 5 | Clearly visible mismatch, typically unacceptable for brand color |
Treat that scale as a decision tool, not a formality. Pull up the Pantone Bridge simulation, soft-proof the file against the ICC profile for the actual substrate, and request a physical press proof on final stock before approving anything above ΔE 2 for a logo or brand mark. A manufacturer’s own color variability standards follow the same logic: measured tolerance, not eyeballed guesswork, decides what passes.
**Pro Tip:** _Write the accepted ΔE tolerance into your production notes, not just your inbox. When a reprint happens six months later on a different substrate, that number is the only thing that keeps the new run honest._
When to Use Pantone vs CMYK for Printing
Matching the method to the job saves money and prevents color complaints after the fact.
- *Logos and brand marks.** Pantone, every time. A logo reprinted slightly warm on one SKU and slightly cool on another erodes shelf recognition faster than almost any other design flaw.
- *Packaging produced across multiple vendors.** Pantone. A specified formula travels between factories in a way a CMYK build file never fully does.
- *Metallics and fluorescents.** Pantone. These are physically outside CMYK’s gamut, not just hard to approximate.
- *Printing on colored, dark, or transparent substrates.** Pantone, generally with an opaque white underprint. CMYK assumes a white base and breaks down without one.
- *Photography and gradient-heavy layouts.** CMYK. Photos need smooth transitions across millions of values, which is what four-color process was built for.
- *Short-run digital printing and large-format graphics.** CMYK. Spot inks require dedicated plates or ink stations that make short runs and oversized formats cost-prohibitive.
- *Everything else, realistically.** A hybrid approach. Many premium packaging jobs run CMYK for imagery plus one or two spot inks for the brand mark, sometimes called five or six-color printing, and it remains one of the most common compromises in commercial print because it protects the one color that matters most without paying spot-ink costs across the whole sheet.
Cost is the tradeoff that decides most of these calls. Spot colors mean extra plates, extra press setup, and often higher minimums, so a five-color job costs more per unit than a four-color one. That premium is easy to justify on a logo and hard to justify on a photograph.
The File Prep and Proofing Workflow That Prevents Reprints
Color failures almost always trace back to a decision made too late in the process, not a flaw in either printing system.
- *Declare your color intent at the start of the file, not the end.** Build in CMYK from the first layout, or flag Pantone spot swatches explicitly in your color palette. Converting a finished file at the last minute is how mismatched blacks and shifted brand colors sneak into production.
- *Soft-proof against the actual printer’s ICC profile**, not a generic monitor preview. Pull the Pantone Bridge simulation for any spot color that will run as CMYK, and calculate the resulting ΔE against your accepted tolerance.
- *Request a physical press or contract proof on the final substrate.** A screen, even a calibrated one, cannot show you how uncoated stock will dull a color or how a metallic ink will catch light. Proper CMYK file preparation, including correct resolution, ink limits, and the right profile, is what keeps that proof meaningful rather than decorative.
- *Document every approval.** Record who signed off, which proof file was approved, the exact ink formula or CMYK build, and the ΔE tolerance. This paperwork is what prevents a “close enough” reprint from happening twice.
**Pro Tip:** _Keep a running color logbook per SKU, not per project. When a bottle label and its matching gift box are produced months apart, that logbook is the only thing standing between a matched set and a customer complaint._
Reviewing your own artwork preparation checklist against this sequence before every handoff catches most color disputes before they reach a press check.
What a Packaging Manufacturer Should Deliver on Color
A supplier’s word on color accuracy is only as good as the process behind it. Some packaging manufacturers build their production process around the same discipline this article recommends: substrate-specific proofing, documented tolerances, and formal sign-off before a job runs at volume. Extensive experience and numerous deliveries support the effectiveness of this approach, which depends on making color decisions on paper rather than by guesswork.
A packaging buyer should expect, at minimum:
- A proof matched to the actual production substrate, not a generic swatch book.
- Explicit Coated or Uncoated selection for every Pantone color specified.
- A stated press profile and a recorded ΔE measurement for the approved match.
- A physical press proof for any brand-critical color, signed off before full production.
Skipping any one of these steps is usually where color inconsistency across SKUs and vendors starts. Requiring them upfront, whether you’re working with custom label printing or a full rigid box program, is what keeps a brand color identical from the first run to the fiftieth.
Why Brand Color Consistency Depends on More Than the Ink
Accuracy in printing has two separate meanings, and mixing them up is where most color complaints start. The first is whether a printed color matches its reference on a given day. The second, and the one that actually protects a brand, is whether that color matches itself run after run, vendor after vendor, year after year. Pantone was built for the second problem. A premixed formula referenced by code doesn’t drift with a new print operator or a different press, because the ink itself is the standard, not a recipe reconstructed from four components every time.
CMYK can be accurate on a given day and still fail at consistency. A perfectly calibrated press today can print a visibly different cyan next month if ink batches change or the substrate lot shifts even slightly. That’s not a flaw in CMYK so much as a structural limit: four variable inks mixed live will always carry more variability than one ink mixed once and shipped as a known quantity.
For single-SKU marketing pieces, that variability rarely matters. For a packaging program running across multiple factories, multiple substrates (folding cartons, rigid boxes, pressure-sensitive labels), and multiple years of reorders, it matters enormously. The brands that treat their logo color as a Pantone-specified constant, checked against a documented ΔE tolerance at every new vendor, are the ones whose shelf presence looks identical whether the box was made in January or made two years and three reprints later.
A Short History of Two Very Different Color Systems
CMYK’s roots trace back to four-color letterpress and offset printing, developed as commercial printing scaled up in the 20th century to reproduce full-color images economically using just four ink stations. The logic was elegant: rather than mixing a unique ink for every color in a photograph, four transparent process inks, layered as dots, could simulate millions of hues. That economy is still why CMYK dominates magazines, photo books, and any full-color imagery today.
Pantone emerged from a different problem entirely. Founded in the 1950s and formalized through the Pantone Matching System in 1963, it addressed a gap CMYK couldn’t close: how does a designer specify an exact color and guarantee a printer anywhere in the world can reproduce it precisely? The answer was a numbered library of premixed spot ink formulas, distributed through physical swatch books, so “Pantone 286 C” meant the same blue whether the job ran in one city or another.
The two systems developed in parallel because they were never solving the same problem. CMYK optimized for economical full-color reproduction. Pantone optimized for portability and exact repeatability of a single, brand-critical color. Modern tools like Pantone Connect and the Color Match Card have digitized parts of that original swatch-book workflow, letting designers capture a physical sample and match it to a Pantone code electronically, but the underlying premise, an ink defined by formula rather than simulated by four components, hasn’t changed since 1963.
Spot Color vs Process Printing: The Technical Divide
The clearest way to separate these systems is by what each ink station actually does. In CMYK, every hue is a calculated blend of four transparent inks, halftoned into dots small enough to fool the eye into seeing a solid color. In Pantone spot printing, one ink station applies one solid, opaque color directly, with no dot pattern required to build the hue.
That structural difference explains almost every practical distinction that follows. Spot inks can carry pigments, like true metallics and fluorescents, that have no CMYK equivalent because there’s no dot combination of cyan, magenta, yellow, and black that produces a metallic sheen. Spot inks also print as flat, solid color with no halftone pattern, which is why fine text and thin logo strokes look crisper in Pantone than in a CMYK build, where the same detail is built from dots that can break up at small sizes.
There’s a real cost to that precision, though. A press running Pantone spot colors needs a dedicated ink station and often a dedicated plate for each spot color used, on top of whatever CMYK stations the job also requires. A five-color job (four process plus one spot) costs more to set up than a straight four-color job, and that premium scales with every additional spot color added. That’s the actual mechanism behind why designers reach for CMYK on cost-sensitive runs and Pantone on jobs where one color’s fidelity outweighs the setup cost.
Why Converting Pantone to CMYK Rarely Works Perfectly
Converting a Pantone solid to its nearest CMYK build is a lossy translation, not a direct equivalent, and the limitations are structural rather than a matter of better software. CMYK’s four inks simply can’t produce every color a single premixed pigment can, which is why over half of all Pantone colors fall at least partially outside the standard CMYK gamut, per Fujifilm’s analysis.
Metallics and fluorescents are the clearest failures: no combination of dots reads as gold foil or neon pink, because those effects rely on physical properties (reflectivity, fluorescence) that transparent process inks don’t have. But plenty of ordinary-looking colors convert poorly too, particularly saturated reds, deep blues, and certain greens that sit at the edges of the CMYK triangle.
Substrate compounds the problem. A Pantone Coated formula assumes ink sitting on a sealed, glossy surface, while an Uncoated formula assumes some absorption into the paper fiber. Convert either one to CMYK without accounting for the actual substrate, and the mismatch compounds: wrong gamut, wrong finish, wrong ink behavior, all stacked into one proof that looks nothing like the reference swatch. Fine patterns and gradients add a third failure mode, since halftone screening at certain angles can produce visible moiré interference that a solid Pantone ink never would.
Choosing the Right Pantone Color for a CMYK-Friendly Result
The best practice here isn’t complicated, it’s disciplined: choose the Pantone color before you choose the printing method, and check its CMYK behavior before you commit to either.
Start with the Pantone Bridge reference for any color that might eventually run as CMYK. If the Bridge simulation looks close to the solid on screen, that’s a candidate for a hybrid approach; if it looks noticeably muted or shifted, that color needs to stay a spot ink regardless of cost. Calculate the ΔE between the solid and its CMYK simulation rather than relying on visual judgment alone, and treat anything above ΔE 2 as a color that should not be approved for CMYK conversion on a brand mark.
Substrate selection matters just as much as the color itself. Choose the Coated or Uncoated Pantone variant that actually matches your production stock, not the one that looks best in a digital swatch book, since the wrong variant causes a visible shift no amount of press skill can correct. And whenever a color needs to hold steady across multiple SKUs or vendors, favor Pantone outright over a CMYK approximation, saving the conversion route for one-off pieces where a small shift carries no brand risk.
How Lighting Changes What You’re Actually Approving
A proof approved under one light source can look wrong under another, and this catches more designers off guard than almost any other variable in the process. Both Pantone spot inks and CMYK builds are affected, but not equally: metallics and fluorescents in a Pantone ink shift dramatically between daylight and warm retail lighting, while a CMYK simulation of the same color can shift in the opposite direction, since its perceived hue depends entirely on how the ambient light interacts with the halftone dots rather than a single pigment.
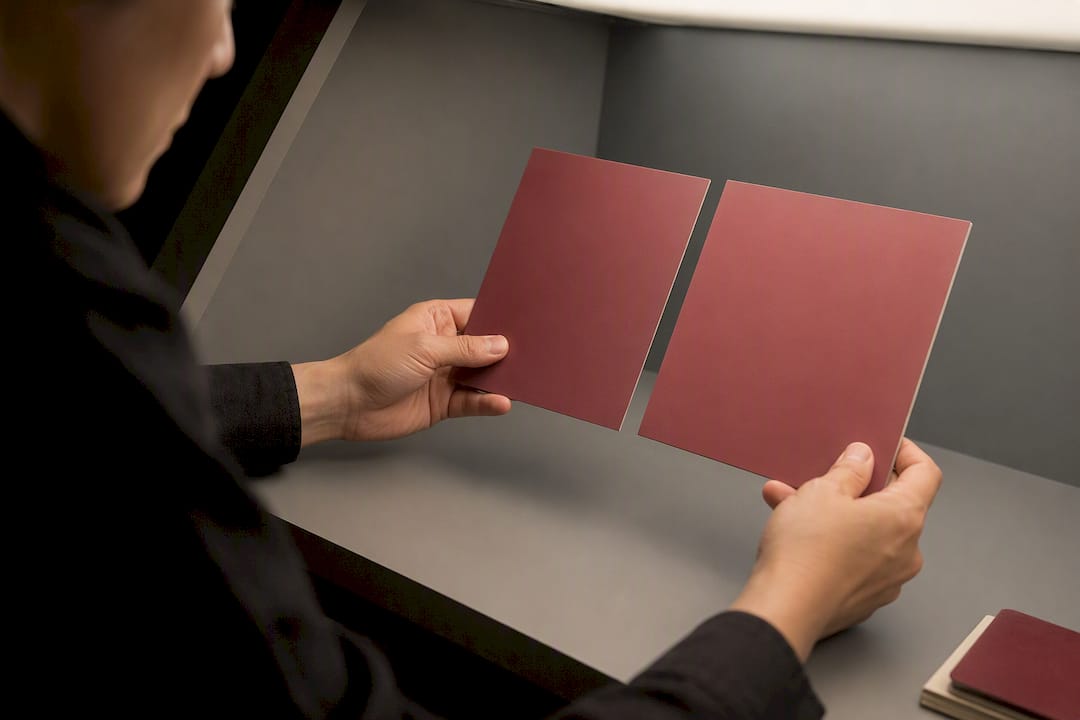
This is why professional color approval happens under standardized viewing conditions, typically a D50 or D65 light booth, rather than under whatever bulb happens to be over the proofing table that day. A color that reads as an acceptable ΔE match under standardized light can still look off under a retail shelf’s fluorescent tubes or a boutique’s warm accent lighting, so packaging destined for a specific retail environment deserves a final check under lighting that resembles where it will actually sit. Skipping this step is how a signed-off proof turns into a shelf surprise weeks later.
Give Your Packaging the Color Fidelity It Deserves
Every principle in this piece points to the same conclusion: a color decision made on paper, with a documented ΔE and a physical proof, always outperforms one made on a screen. That’s the standard Yuanpackaging builds into every production run, whether the job is a run of cosmetic labels that need an exact metallic gold to match a brand’s hero product, or a batch of wine and spirits labels where a single Pantone shift across vendors would be immediately visible on a store shelf. If your next packaging program needs brand color that holds up across factories, substrates, and reorders, explore Yuanpackaging’s full product range and start the conversation with a substrate-matched proof, not a guess.
What This Debate Gets Wrong
Most guidance on Pantone versus CMYK treats it as a philosophical choice, brand purity against production economics, when it’s really an engineering decision with a measurable answer. ΔE gives you a number. Substrate gives you a constraint. Neither leaves much room for opinion once you’ve actually run the proof.
Where I think the conventional advice falls short is in treating “use Pantone for brand colors” as the end of the conversation. It’s the start of one. Specifying Pantone 286 C means nothing if nobody documents whether the approved proof was Coated or Uncoated, what press profile generated it, or what ΔE tolerance was actually accepted. I’ve seen more color disputes come from missing paperwork than from an actual ink failure.
If you take one thing from this, take this: treat the ΔE number and the substrate as fixed facts before you argue about aesthetics. A designer who insists on Pantone without checking gamut fit is gambling on cost. A production team that defaults to CMYK without soft-proofing against the real substrate is gambling on brand consistency. The fix for both is the same unglamorous habit: proof it, measure it, write it down.
_— Anthony_
Sources
- Pantone vs CMYK — PantoneTools learning article
- What is Delta E and why is it important for color accuracy? — ViewSonic
- Pantone vs CMYK — Fujifilm Print US
FAQ
Should I use Pantone or CMYK for my print job?
Use Pantone for brand-critical colors, metallics, fluorescents, or printing on colored or uncoated substrates, and use CMYK for photography, gradients, and full-color imagery where minor shifts won’t be noticed.
How do I match CMYK to a Pantone color?
Check the Pantone Bridge guide for the nearest CMYK simulation, then soft-proof against your printer’s ICC profile and calculate the ΔE; anything under 2 is generally safe, while anything above 5 is a visible mismatch.
Why do some Pantone colors look strange or hard to reproduce in CMYK?
Certain Pantone solids, including metallics, fluorescents, and some saturated blues, reds, and greens, fall at least partially outside the standard CMYK gamut, so no combination of four process inks can fully match them.
Is Pantone outdated now that digital color tools exist?
No. Digital tools like Pantone Connect have modernized how designers capture and reference colors, but the core system, premixed spot inks defined by formula, remains the standard for guaranteeing exact, repeatable brand color across presses and vendors.